



Metal milling is already one of the more demanding areas in dental CAD/CAM. Compared with softer dental materials, titanium requires more stable cutting control, stronger machine rigidity, appropriate toolpaths, and careful management of tool wear. But even within metal milling, not all cases are equally difficult.
A single titanium abutment or small metal component is challenging in its own way. An implant bar is a different level of difficulty.
Implant bar milling is more demanding because the case is larger, longer, more rigidly defined by implant positions, and less forgiving of distortion or fit deviation. The workflow has to maintain accuracy across a broader structure, manage heavier cutting load, protect connection areas, and preserve passive fit across multiple implants.
That is why implant bar milling should not be judged by the same standard as single-unit metal work. A lab may be able to mill smaller titanium components successfully, but implant bars require a more controlled workflow from scan data and CAD design all the way to CAM strategy, machine stability, tool condition, and finishing.
Implant bars are larger and less forgiving
The first difference is simple: an implant bar is usually much larger than a single metal component.
A larger case creates more variables during milling. There is more material to remove, more surface area to control, more time under cutting load, and more opportunity for small errors to accumulate. A single-unit component may be affected by local variation, but an implant bar has to remain accurate across its full length.
This matters because implant bars must connect to multiple implant positions. Even a small deviation in one area can influence how the full structure seats.
In single-unit work, a small local issue may be easier to correct or may only affect one restoration. In an implant bar, the geometry is connected. One weak area can influence the whole fit relationship.
That is why implant bar milling demands not just accuracy, but consistency across the entire structure.
Passive fit makes implant bar milling more demanding
One of the most important reasons implant bars are difficult is the need for passive fit.
In implant-supported restorations, the bar should seat accurately without creating unwanted stress on the implants or prosthetic components. This is different from a single-unit case, where fit is usually evaluated within a smaller local relationship.
For implant bars, the challenge is broader. The bar must align with multiple implant interfaces, maintain correct spacing, and preserve the designed relationship between all connection points.
This requires reliable control over:
-
implant interface geometry
-
screw channel position
-
bar length and shape
-
milling accuracy across multiple axes
-
distortion risk during cutting
-
finishing around connection areas
If the bar does not seat passively, the problem is rarely simple. It may come from scan data, CAD design, CAM compensation, milling strategy, machine stability, or post-milling handling. That makes diagnosis and correction much harder.
This is why implant bar milling is not just “larger metal milling.” It is a fit-critical workflow.
Multi-implant alignment increases the risk of accumulated error
Single-unit metal work usually depends on one main seating relationship. Implant bars depend on several.
Each implant position must be represented correctly in the digital workflow, and the final milled bar must respect all of them at once. This means small errors can accumulate across the case.
For example, if scan data is slightly unstable, CAD design is slightly overcompensated, CAM strategy applies uneven finishing, or the machine loses consistency under load, the final bar may still look acceptable visually but fail to seat as expected.
The difficulty is that implant bar errors are often not obvious until try-in. A surface may appear smooth, and the overall shape may look correct, but the fit relationship across multiple implants may still be wrong.
That is why implant bar workflows require more careful validation than many single-unit cases. The question is not only whether the bar looks right. The question is whether the entire structure remains dimensionally reliable.
Titanium cutting load is more difficult to manage in long-span structures
Titanium is widely used for implant-related restorations because of its strength, biocompatibility, and clinical relevance. But from a milling perspective, titanium is not an easy material.
It can generate higher cutting forces, increase tool wear, and demand stable chip evacuation and thermal control. In a larger implant bar, these challenges become more important because the machine must maintain stability over a longer and more demanding job.
Compared with single-unit work, implant bar milling often involves:
-
longer milling time
-
larger volume of material removal
-
heavier cutting load
-
more continuous tool engagement
-
more sensitive finishing requirements
-
higher consequence if accuracy drifts
If the machine lacks rigidity, or if the toolpath creates unstable cutting conditions, the bar may show chatter, tool marks, dimensional inconsistency, or fit issues.
This is where a dedicated titanium milling workflow becomes important. Implant bars are not ideal cases for a workflow that is only barely capable of cutting titanium. They require a system that can maintain control throughout the full job.
Machine rigidity matters more as the case gets larger
Machine rigidity is important in any metal milling workflow, but implant bars make it especially critical.
When cutting titanium, the machine has to resist vibration and maintain precise motion under load. If the machine structure, spindle, fixture, or axis control is not stable enough, the result may show visible or hidden quality problems.
For implant bars, instability may appear as:
-
chatter marks on long surfaces
-
inconsistent finish around connection areas
-
slight dimensional variation across the bar
-
tool marks that are difficult to polish out
-
fit issues that are hard to trace to one single point
The longer and more complex the structure, the more important stability becomes.
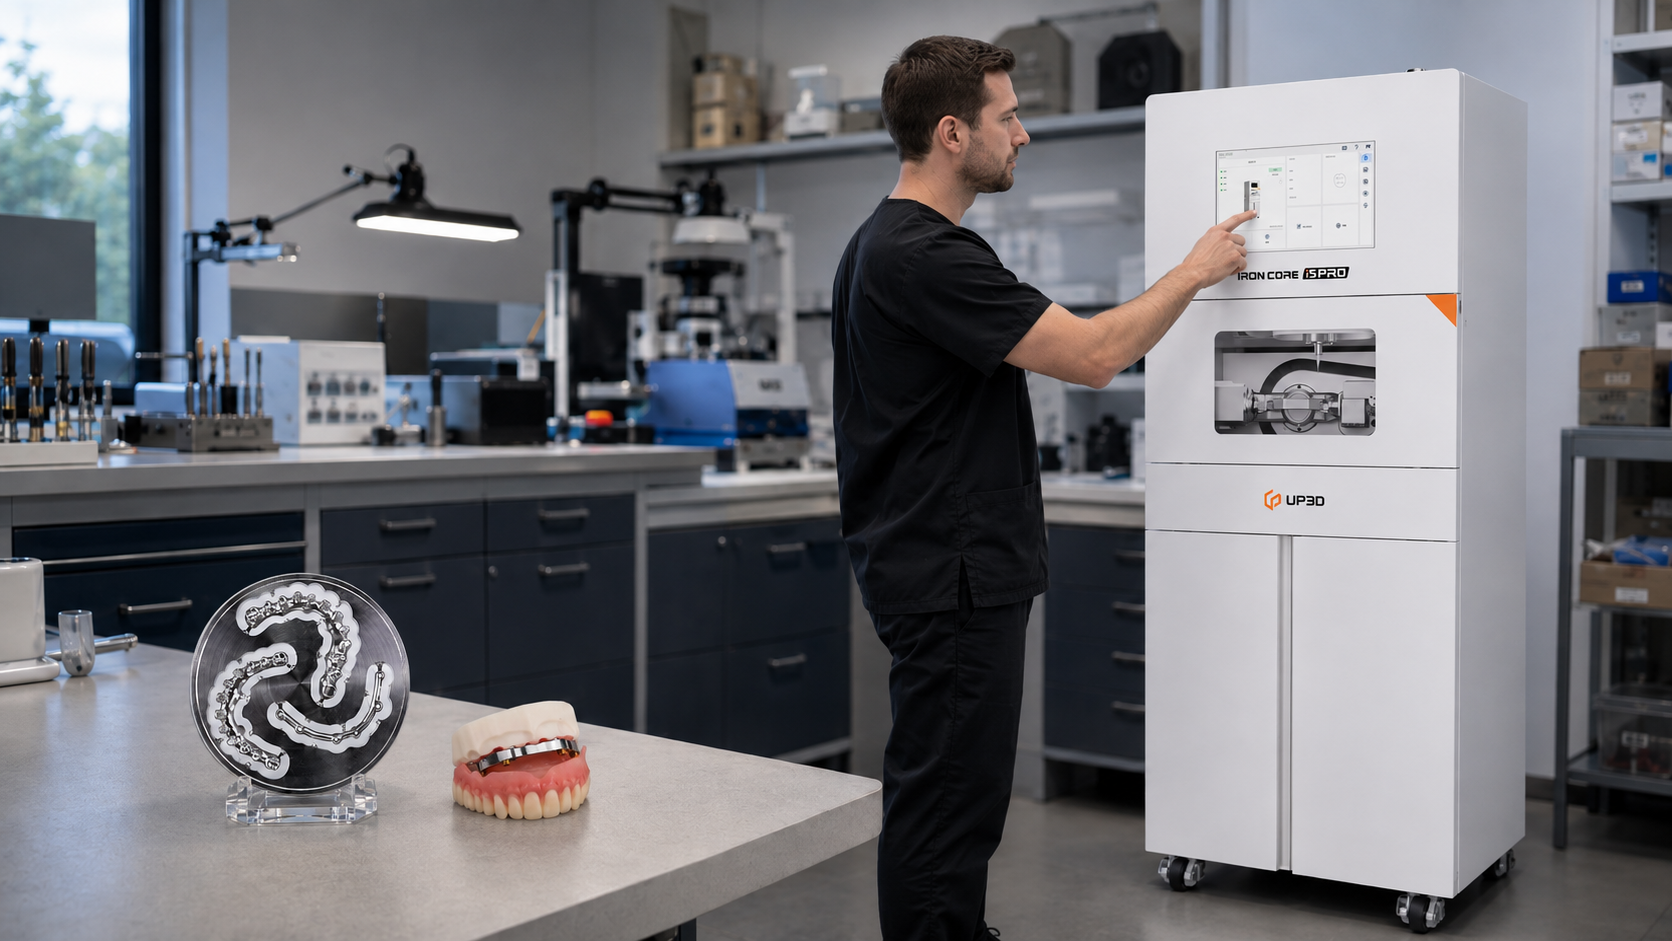
This is one reason titanium milling platforms such as IRON CORE i5 PRO are relevant for labs working with implant components. The value is not only the ability to mill titanium, but the ability to support a more stable workflow for demanding implant-related cases where rigidity and repeatability matter.
CAM strategy must protect both efficiency and accuracy
Implant bar milling cannot rely on a generic metal toolpath.
The CAM strategy has to manage cutting load, tool engagement, finishing allowance, support strategy, and surface quality. If the CAM is too aggressive, the job may create vibration, tool stress, or surface defects. If the strategy is too conservative, production time may become inefficient without necessarily improving fit.
The challenge is balance.
A good CAM strategy for implant bars should consider:
-
roughing efficiency without excessive tool load
-
stable finishing passes
-
protection of implant interface areas
-
smooth transitions around long surfaces
-
tool access to internal and external geometry
-
appropriate support and positioning
-
realistic machining of fine features
This is why CAM preparation matters as much as machine capability. Even a rigid machine can produce poor results if the toolpath is unstable or poorly matched to the material and case geometry.
For implant bars, CAM is not just a production step. It is part of the accuracy strategy.
Tool wear becomes more critical in implant bar cases
Tool wear affects all milling workflows, but implant bars make tool condition especially important.
A worn tool may still produce an acceptable result on a smaller or less demanding case. But in titanium implant bar milling, tool wear can create more serious problems because the job is longer, the material is tougher, and the required fit is more demanding.
Tool wear may lead to:
-
rougher surface finish
-
increased heat and friction
-
more cutting resistance
-
loss of fine detail
-
reduced consistency in finishing passes
-
higher risk of chatter or tool marks
If a tool is already close to the end of its effective life, an implant bar may expose that weakness quickly.
This is why labs should not manage tool life only by counting jobs. They should consider material type, case size, cutting time, and the quality requirement of the case. A high-value implant bar should not be treated like a routine low-risk job when deciding whether a bur is still suitable.
Connection areas are more sensitive than general bar surfaces
Not all parts of an implant bar have the same importance.
Large external surfaces matter for finish and hygiene, but implant connection areas are even more critical because they determine how the bar seats and interfaces with the implant components.
These areas require careful control during:
-
CAD design
-
CAM strategy
-
tool selection
-
finishing
-
inspection
Over-polishing, poor tool access, unstable milling, or incorrect finishing around connection areas can create fit problems even if the rest of the bar looks good.
This is one major difference between implant bar milling and general single-unit metal work. In a single component, the critical area is smaller and easier to isolate. In an implant bar, multiple connection points must all remain accurate in relation to each other.
That makes the workflow less tolerant of small mistakes.
Long-span geometry is harder to support during milling
Implant bars often have long, irregular geometries. They may include curves, screw access channels, framework extensions, and varying thickness across the structure.
This creates support challenges during milling.
If the bar is not positioned and supported properly, the milling process may introduce vibration, stress, or unwanted movement. Even small instability can affect the final result.
Good nesting and support planning should help protect:
-
long-span areas
-
thin transitions
-
connection zones
-
screw channel regions
-
surfaces that require clean finishing
This is another reason implant bar milling requires more experience than single-unit metal work. The case must be prepared in CAM with the full milling process in mind, not just placed into the material and sent to the machine.
Surface finish matters for both function and finishing time
Implant bars require a clean surface not only for appearance but also for function, hygiene, and downstream finishing.
Poor surface quality can increase finishing time and make the final result less predictable. In titanium cases, aggressive manual finishing can also create risks if critical areas are affected.
Surface problems in implant bar milling may come from:
-
tool wear
-
unstable cutting
-
poor CAM finishing strategy
-
insufficient rigidity
-
heat or chip evacuation issues
-
inappropriate tool engagement
For single-unit cases, minor surface issues may be easier to correct. For implant bars, the surface area is larger and the geometry is more complex, so additional finishing can become time-consuming and risky.
A stable milling workflow should aim to reduce the need for heavy correction after milling.
Milling time is longer, so process stability matters more
Implant bar jobs usually take longer than single-unit metal cases. A longer job means the workflow has to stay stable for a longer period of time.
This creates more demand on:
-
spindle performance
-
tool condition
-
machine temperature stability
-
cutting load control
-
coolant or chip management depending on workflow
-
CAM consistency
-
operator monitoring
A small instability that appears late in the job can still affect the final result. This is one reason process reliability is so important.
In high-value implant cases, the cost of failure is not only material waste. It also includes lost machine time, technician time, possible remake, and delayed delivery.
For labs, stable implant bar milling is ultimately a productivity issue as much as a quality issue.
Inspection is more demanding than visual review
A single-unit metal component can often be judged with a combination of visual inspection, fit check, and surface review. Implant bars require more careful evaluation because problems may not be obvious from appearance alone.
A bar can look clean but still have a seating issue. It can have good surface finish but still fail to achieve the expected passive fit. It can appear accurate in one area but show a small mismatch across another implant position.
This is why implant bar workflows should include careful inspection habits, especially around:
-
connection points
-
screw channels
-
bar seating
-
interface geometry
-
long-span distortion
-
surface quality after finishing
The more demanding the case, the less the lab should rely on appearance alone.
Implant bar milling requires an integrated workflow
The difficulty of implant bar milling is that no single stage can guarantee success by itself.
Accurate scan data is important, but it is not enough.
Good CAD design is important, but it is not enough.
A strong CAM strategy is important, but it is not enough.
A rigid milling machine is important, but it is not enough.
The workflow succeeds when all of these elements work together.
That includes:
-
reliable implant position data
-
careful bar design
-
appropriate titanium milling strategy
-
stable machine performance
-
correct tool management
-
controlled finishing
-
clear inspection standards
This is where a dedicated solution approach becomes valuable. For labs moving into in-house titanium implant bar production, systems such as IRON CORE i5 PRO can serve as part of a more controlled metal milling workflow, especially when paired with appropriate CAM strategy, tool management, and case validation habits.
The goal is not simply to mill metal. The goal is to produce implant components with repeatable fit and confidence.
Why single-unit success does not always mean implant bar readiness
A lab that can mill single-unit titanium components successfully may still need to evaluate whether it is ready for implant bar production.
The workflow requirements are different.
Before taking on implant bars, a lab should consider:
-
whether the machine can maintain stability under longer titanium jobs
-
whether the CAM strategy is suitable for bar geometry
-
whether tool life is being tracked properly
-
whether technicians understand passive fit requirements
-
whether finishing procedures protect connection areas
-
whether the lab has a consistent inspection process
This does not mean implant bar milling is out of reach. It means it should be approached as a higher-level workflow, not simply an extension of smaller metal milling cases.
Final Thoughts
Implant bar milling is more difficult than single-unit metal work because it combines several demanding factors at once: titanium cutting load, long-span geometry, multiple implant positions, passive fit requirements, connection-area precision, longer milling time, and higher consequences if accuracy drifts.
A single-unit metal component mainly tests local accuracy. An implant bar tests the stability of the entire workflow.
That is why successful implant bar milling depends on more than the ability to cut titanium. It requires clean data, careful CAD design, suitable CAM strategy, strong machine rigidity, controlled tool wear, precise finishing, and reliable inspection.
For dental labs, this is the key mindset shift: implant bar milling is not just metal milling at a larger size. It is a fit-critical implant workflow. The labs that understand this difference are better prepared to produce titanium implant bars with consistency, confidence, and fewer costly surprises.


